Indexable drills
From Ø12.5 to Ø60 mm, depth 2D–5D. The insert wears out, not the tool: the body lasts for years and the cost per hole falls several times over compared with solid carbide of the same diameter.
We reply within the working day. There is no minimum order.
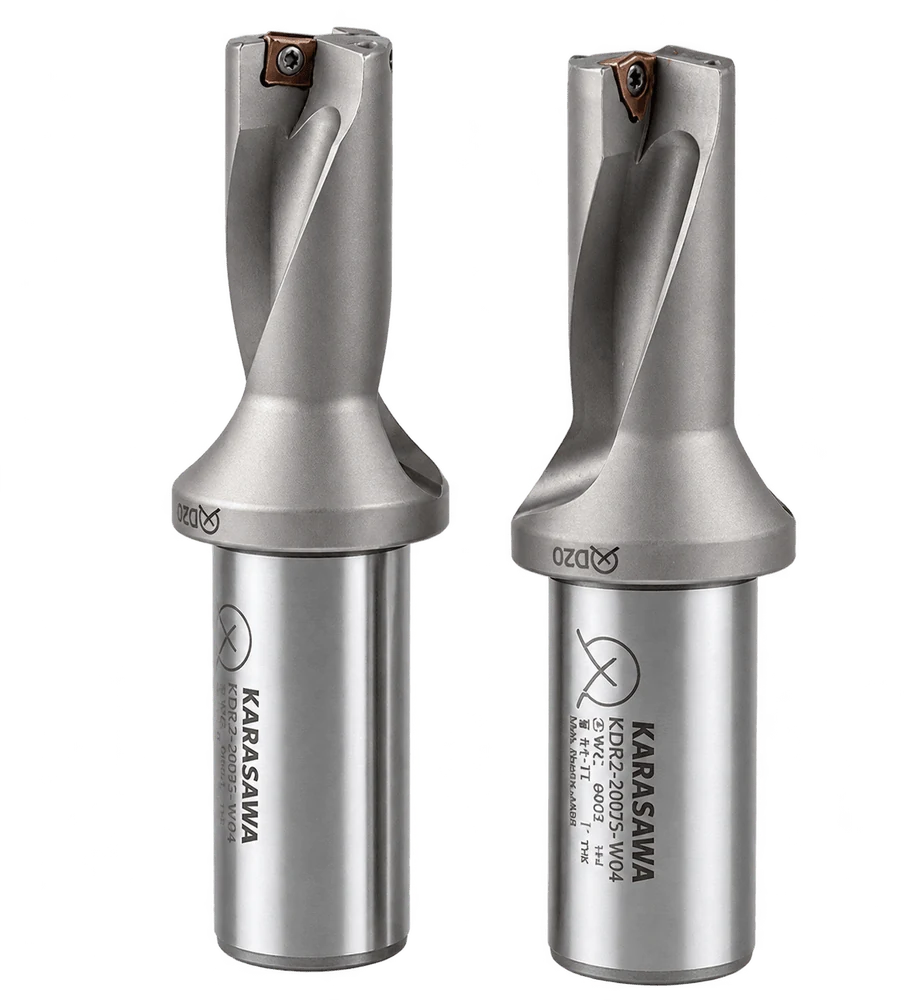
Model range
An indexable insert changes the logic of the tool: the drill stops being a consumable and becomes equipment. You buy the body once, after that only inserts follow — and at Ø30 the difference in cost per hole against a solid drill is already visible over the first hundred parts.
The second advantage is speed. An indexable insert removes 2–3 times more metal per minute than a solid drill of the same diameter, because it is not afraid of edge heating: a hot insert is simply indexed to a fresh corner.
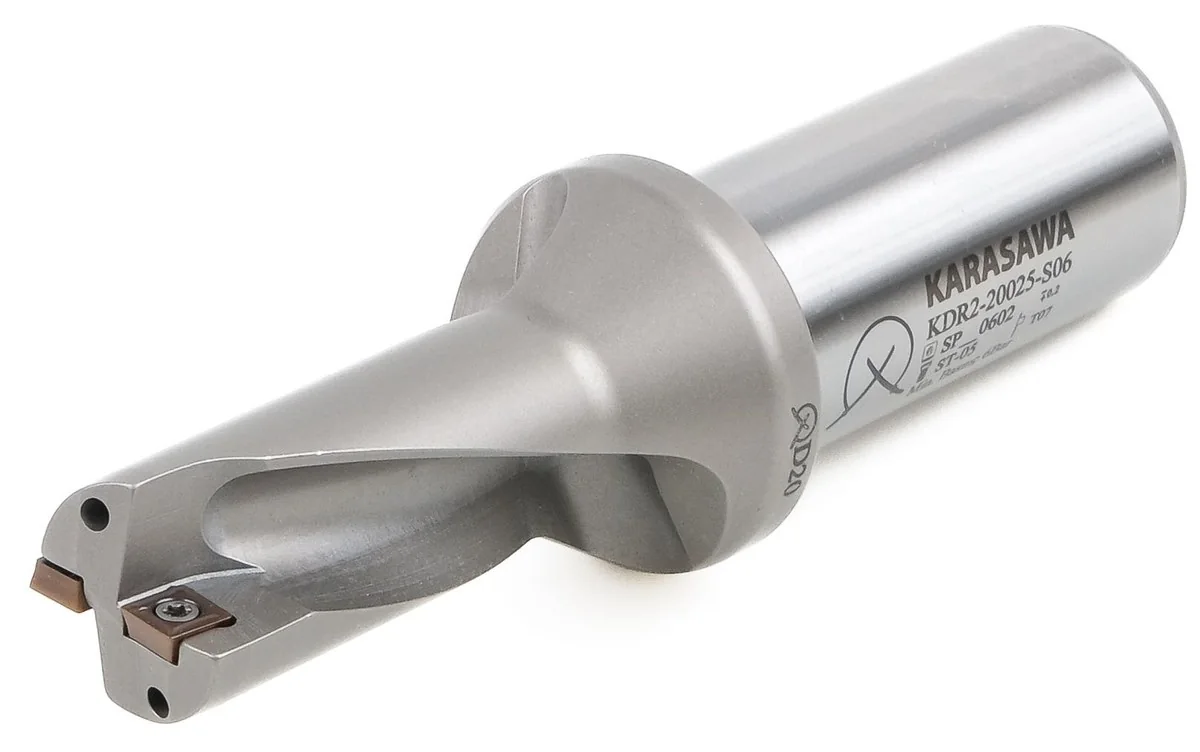
KDR2-20025-S06 · insert SP..0602 · screw ST-05 · key T07The base series for steel, cast iron and non-ferrous metals. The square insert gives four cutting edges: when the first one dulls, the insert is indexed — four times over before it is replaced.
Chipbreaker geometries: M — universal, for steel and cast iron; S — sharp, for aluminium and ductile materials where an ordinary edge only pushes; R — with a reinforced edge, for severe conditions and uneven stock.
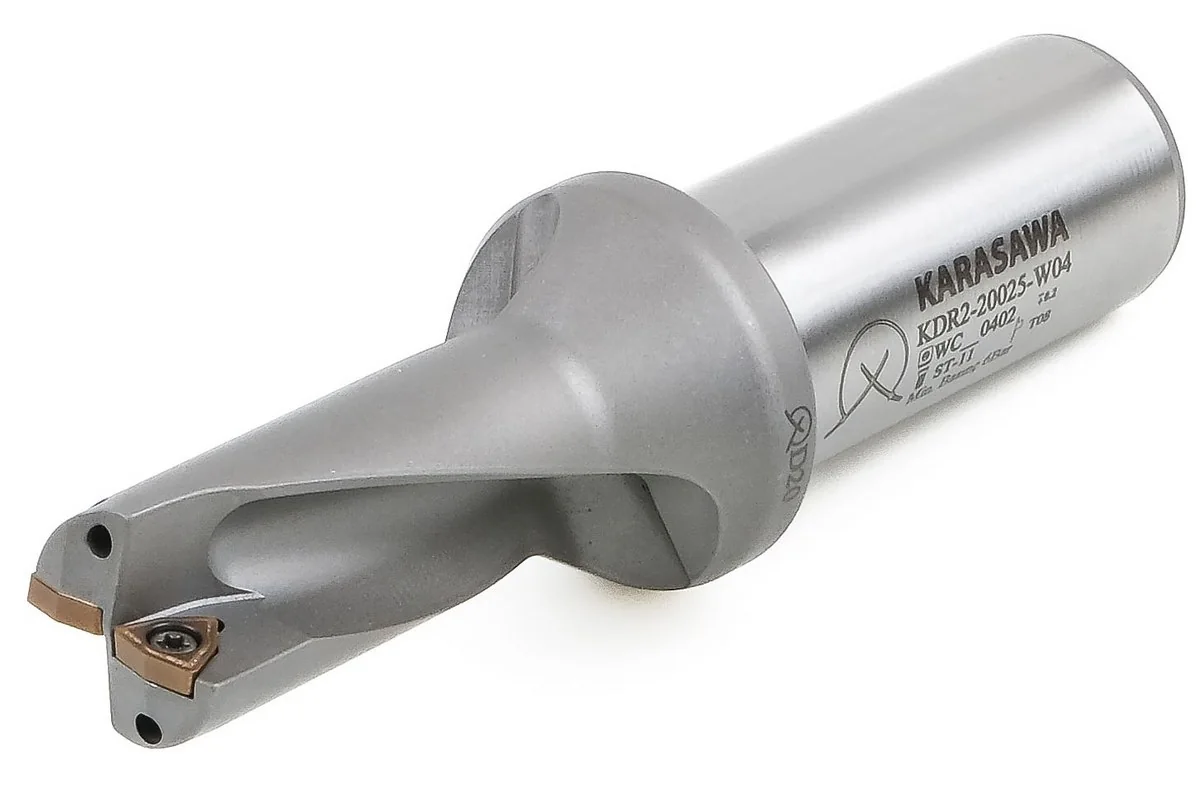
KDR2-20025-W04 · insert WC..0402 · screw ST-11 · key T08The widest range in the line — up to Ø60 mm. The trigon insert with its reinforced corner angle takes impact better than a square one, which is why this series is the one for stainless, heat-resistant alloys and interrupted cutting: castings with scale, holes in inclined surfaces, breaking into a cavity.
Where a KDR-S chips its edge on the very first entry into the material, a KDR-W takes the batch to the end.
Grades and coatings
The drill body sets the geometry and the rigidity — and there its role ends. Everything else is decided by the insert: how many holes it will do, whether it will survive entering a casting with scale, whether ductile stainless will start welding itself to the edge.
The KARASAWA programme has three grades for hole-making tools. All three are on an AlTiSiN PVD coating: nanolayer structure, working temperature up to 1200 °C, coefficient of friction 0.3–0.4. What separates them is the substrate — the balance of hardness and toughness, that is, what the insert minds less: wear or impact.
In practice it looks like this: if the edge wears evenly, fit a more wear-resistant grade; if it chips, fit a more impact-resistant one, even at the cost of slightly shorter life in a smooth cut.
| Grade | Colour | Coating | Character | P | M | K | N | S | H | Where this works |
|---|---|---|---|---|---|---|---|---|---|---|
| PM3215wear-resistant | PVD AlTiSiN | Hard substrate, maximum resistance to wear and corrosion | ● | ○ | ● | — | — | ○ | Long stable batches in carbon and alloy steel and cast iron. Uninterrupted cutting, a rigid machine, predictable stock. Moulds and dies, automotive components, general engineering. | |
| MS3265universal | PVD AlTiSiN | A balanced substrate: it handles both wear and moderate impact | ● | ○ | ● | ○ | ○ | ● | The first choice for a mixed range of work: steel, cast iron, hardened material, and with the S geometry aluminium and brass. If one grade has to cover every job on the shop floor, this is it. | |
| MS4265impact-resistant | PVD AlTiSiN | Tough substrate, high resistance to impact loading | ○ | ● | ○ | — | ● | — | Stainless, titanium, nickel alloys, interrupted cutting, castings with scale and skin. Where the previous grade does not wear away but chips along the edge. Aerospace, medical parts, electronics. |
The other half of the decision is the chipbreaker geometry. The same grade with the index M, S or R behaves differently: M is a universal edge with a reinforced chamfer for steel and cast iron; S is a sharp edge with a small edge radius for stainless, titanium and aluminium, where a blunt edge does not cut but work-hardens the material; R is a reinforced edge for severe conditions: castings with scale, uneven stock, interrupted cutting. The right pairing is always “grade + geometry”, never the grade on its own.
Selection
A table for indexable drilling with a hole tolerance of −0.1…+0.4 mm. Written as: body series · insert with geometry · grade.
| Material group | Examples | First recommendation | Second recommendation | What to watch for |
|---|---|---|---|---|
| Psteel | S235, C45, 42CrMo4, cast steel | KDR-S · SPMK-M · MS3265 | KDR-W · WCMK-M · MS3265 | The classic case. As the drill breaks through the part, reduce the feed over the last 2–3 mm — otherwise that is exactly where the insert chips. |
| Mstainless | AISI 304, 316, 321, duplex | KDR-W · WCMK-S · MS4265 | KDR-S · SPMK-S · MS3265 | The sharp S geometry is essential. Coolant at no less than 20 bar — otherwise the chip stays in the hole and ruins the insert. |
| Kcast iron | Grey, ductile and malleable cast iron | KDR-S · SPMK-M · MS3265 | KDR-W · WCMK-M · MS3265 | A casting with scale is a case for the KDR-W: the trigon insert copes better with entering an uneven surface. |
| Naluminium, brass | 2024 aluminium, AlSi, bronze, brass | KDR-S · SPMK-S · MS3265 | — | An SPMK insert with a sharp polished edge. The main problem is adhesion: keep the feed high and do not let chips build up. |
| Sheat-resistant, titanium | Inconel, Ti-6Al-4V, Hastelloy | KDR-W · WCMK-S · MS4265 | KDR-S · SPMK-M · MS4265 | The cutting speed is low, the feed is not. Plan the edge change by running time, not by “while it still cuts”: on these materials failure comes suddenly. |
| Hhardened steel | Tool steel after heat treatment | KDR-S · SPMK-M · MS3265 | KDR-W · WCMK-M · MS3265 | The rigidity of the system decides everything. Keep the drill overhang to a minimum and the body runout within 0.03 mm. |
M — universal chipbreaker geometry (steel, cast iron). S — sharp (stainless, titanium, non-ferrous). R — reinforced (severe conditions, castings with scale). The figure in the body code is the depth in diameters.
In summary
An indexable drill is rarely bought “to make things better”. It is bought when solid carbide at a large diameter becomes a noticeable cost — and this is what the difference is made of.
The body outlives hundreds of inserts. A worn Ø30 solid drill is a whole piece of spent carbide; here only the insert is spent, and it still has three unused edges.
The insert is changed right at the machine. There is no need to send the tool out for regrinding, wait for the grinder and set the overhang again — the hole axis stays where it was.
Two body series and two insert types cover the Ø12.5–60 mm range. Instead of two dozen solid drills of different diameters — a compact and predictable stock.
